DIN VDE 0250 / IEC 60245 / IEC 60092 / UL Compliant Engineering

Custom Cable Engineering & OEM Manufacturing Services

TEBAOFLEX engineers and manufactures custom flexible rubber, reeling, mining, marine, and high-temperature cables from 0.6/1 kV up to 35 kV. We convert equipment load parameters, customer drawings, or existing sheath markings into verified cable constructions with routine high-voltage test reports and ISPM-15 export drum packing.

0.6/1 kV – 35 kV Low & medium voltage flexible rubber and reeling cables
Class 5 & Class 6 IEC 60228 bare or tinned fine-stranded copper conductors
-50°C to +180°C EPR, HEPR, XLPE, Silicone, PCP, CSP & PUR compounds

Five-Layer Custom Cable Construction Capabilities

Custom cable design at TEBAOFLEX covers five structural layers: conductor stranding, dielectric insulation, hybrid core assembly, tensile or electromagnetic shielding, and heavy-duty elastomeric sheathing. Engineers can specify each layer independently to match voltage drop limits, dynamic reeling stress, and international safety standards.

Cable LayerCustomizable OptionsEngineering Range & PerformanceReference Standards
01. Conductor Current & Flex LifeFinely stranded bare annealed copper or tinned copper (corrosion & sulfide resistant); rope-lay bunching with reverse-lay pitch for torsional balance.Cross-sections from 0.5 mm² to 400 mm²; single-core feeder up to 61-core control configurations.IEC 60228 Class 5 / Class 6
DIN VDE 0295
02. Insulation & Semicon Dielectric & ThermalEthylene Propylene Rubber (EPR / HEPR), XLPE, Silicone Rubber, or fluoropolymer (PFA/FEP); triple-extruded inner/outer semiconductive screens for MV cables.Rated voltages from 300/500 V, 0.6/1 kV, 3.6/6 kV, 6/10 kV up to 18/30 kV (35 kV); continuous conductor temp up to +90°C or +180°C.DIN VDE 0207
IEC 60502 / UL 62
03. Core & Hybrid Assembly Power + Signal + FOComposite core lay-up combining 3 phases + split earth (3+3E), pilot/monitoring cores, twisted-pair RS485/CANbus data pairs, or embedded fiber-optic tubes.6/12/24-core single-mode (G.652D / G.657A) or multi-mode optical fibers in gel-filled loose tubes with central elastomers.DIN VDE 0250-814
IEC 60794
04. Tensile & EMC Shielding Anti-Torsion & ScreeningCentral aramid (Kevlar) load-bearing core, anti-torsion synthetic yarn open braid between inner/outer sheaths, individual/overall tinned copper braid, or galvanized steel wire braid (GSWB).Permanent tensile load capacity 15 N/mm² to 30 N/mm²; ≥85% optical coverage copper screening for VFD & EMC immunity.DIN VDE 0250-812
IEC 60092-350
05. Inner & Outer Sheath Environmental ArmorPolychloroprene (PCP / Neoprene), Chlorosulfonated Polyethylene (CSP / Hypalon), Chlorinated Polyethylene (CPE), Polyether Polyurethane (PUR), or SHF2 mud-resistant LSZH.Operating ambient -50°C to +90°C; oil resistance (EN 60811-404), flame retardancy (IEC 60332-1-2 / 60332-3), hydrostatic water pressure up to 100 bar.IEC 60245 (53/57/66)
NEK 606 / EN 50525

End-to-End Project Support Across Engineering, OEM & Logistics

TEBAOFLEX integrates cable structure design, private-label OEM manufacturing, high-voltage laboratory verification, and export container loading within a single manufacturing base. This eliminates specification mismatches between third-party traders and workshop production lines.

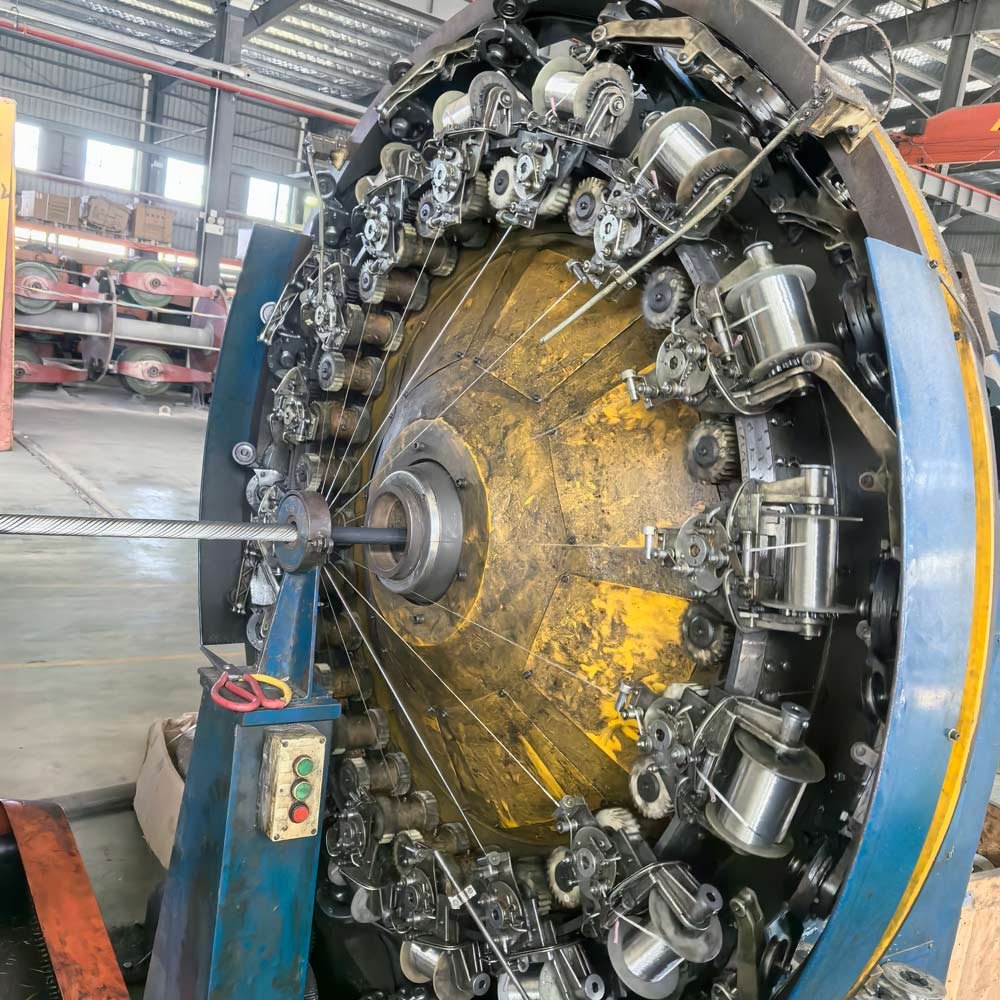
High-speed steel wire and copper braiding machine in TEBAOFLEX cable workshop Structure & Replacement Design

Technical Selection & Reverse Engineering

Before issuing a commercial quote, our engineers verify conductor ampacity, short-circuit withstand capability, dynamic bending radius, and sheath compatibility against your site equipment.

  • 2D cross-section CAD drawing & BOM sheet prior to order confirmation
  • Direct cross-reference from existing European, American, or Japanese cable codes
  • Custom small-batch prototyping for OEM machinery trials
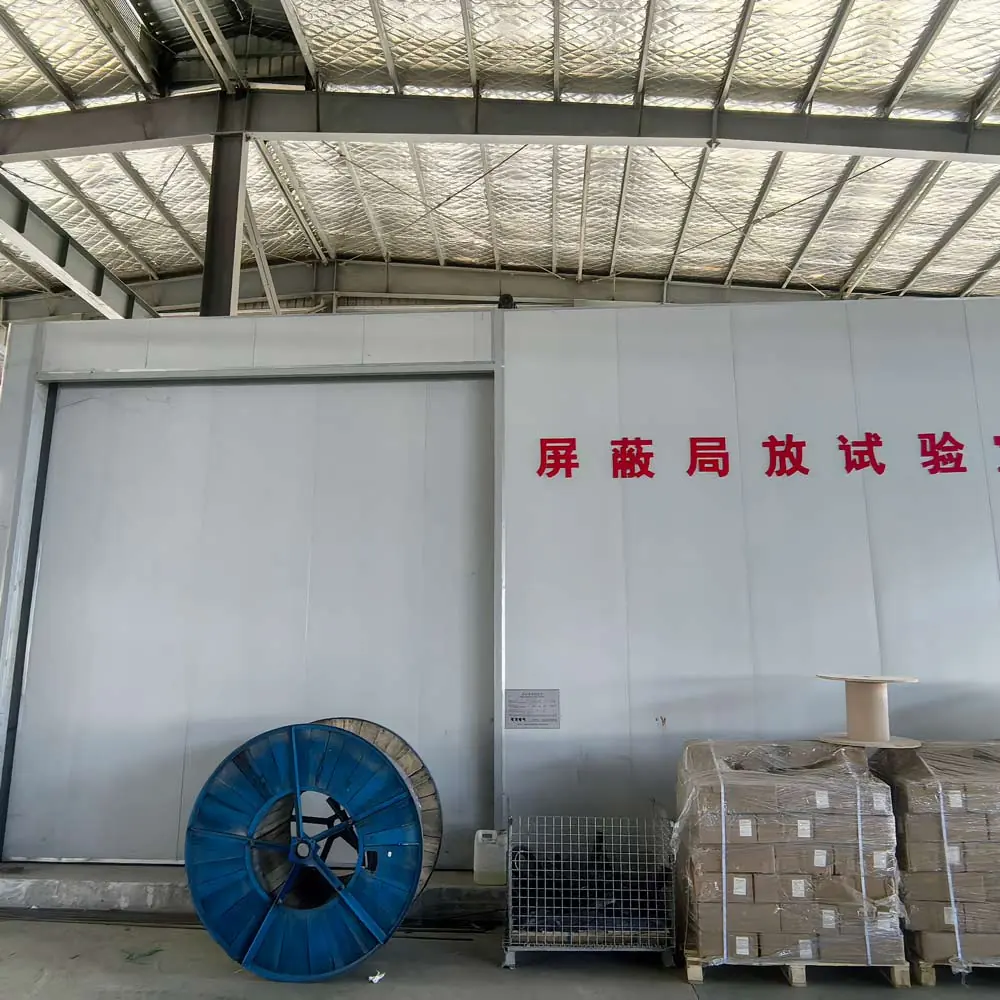
High-voltage partial discharge shielded testing laboratory at TEBAOFLEX Routine Testing & Certification

In-House HV Testing & Quality Traceability

Every production drum undergoes mandatory factory routine inspections in our laboratory, including conductor DC resistance, AC high-voltage dielectric testing, partial discharge, and sheath mechanical elongation tests.

  • Batch-specific Factory Acceptance Test (FAT) & routine inspection reports
  • Verified compliance with TÜV Rheinland (J 50687206), UL/cUL (E556567), CE & ISO 9001
  • Pre-shipment sample retention and third-party witness inspection support (SGS / BV)
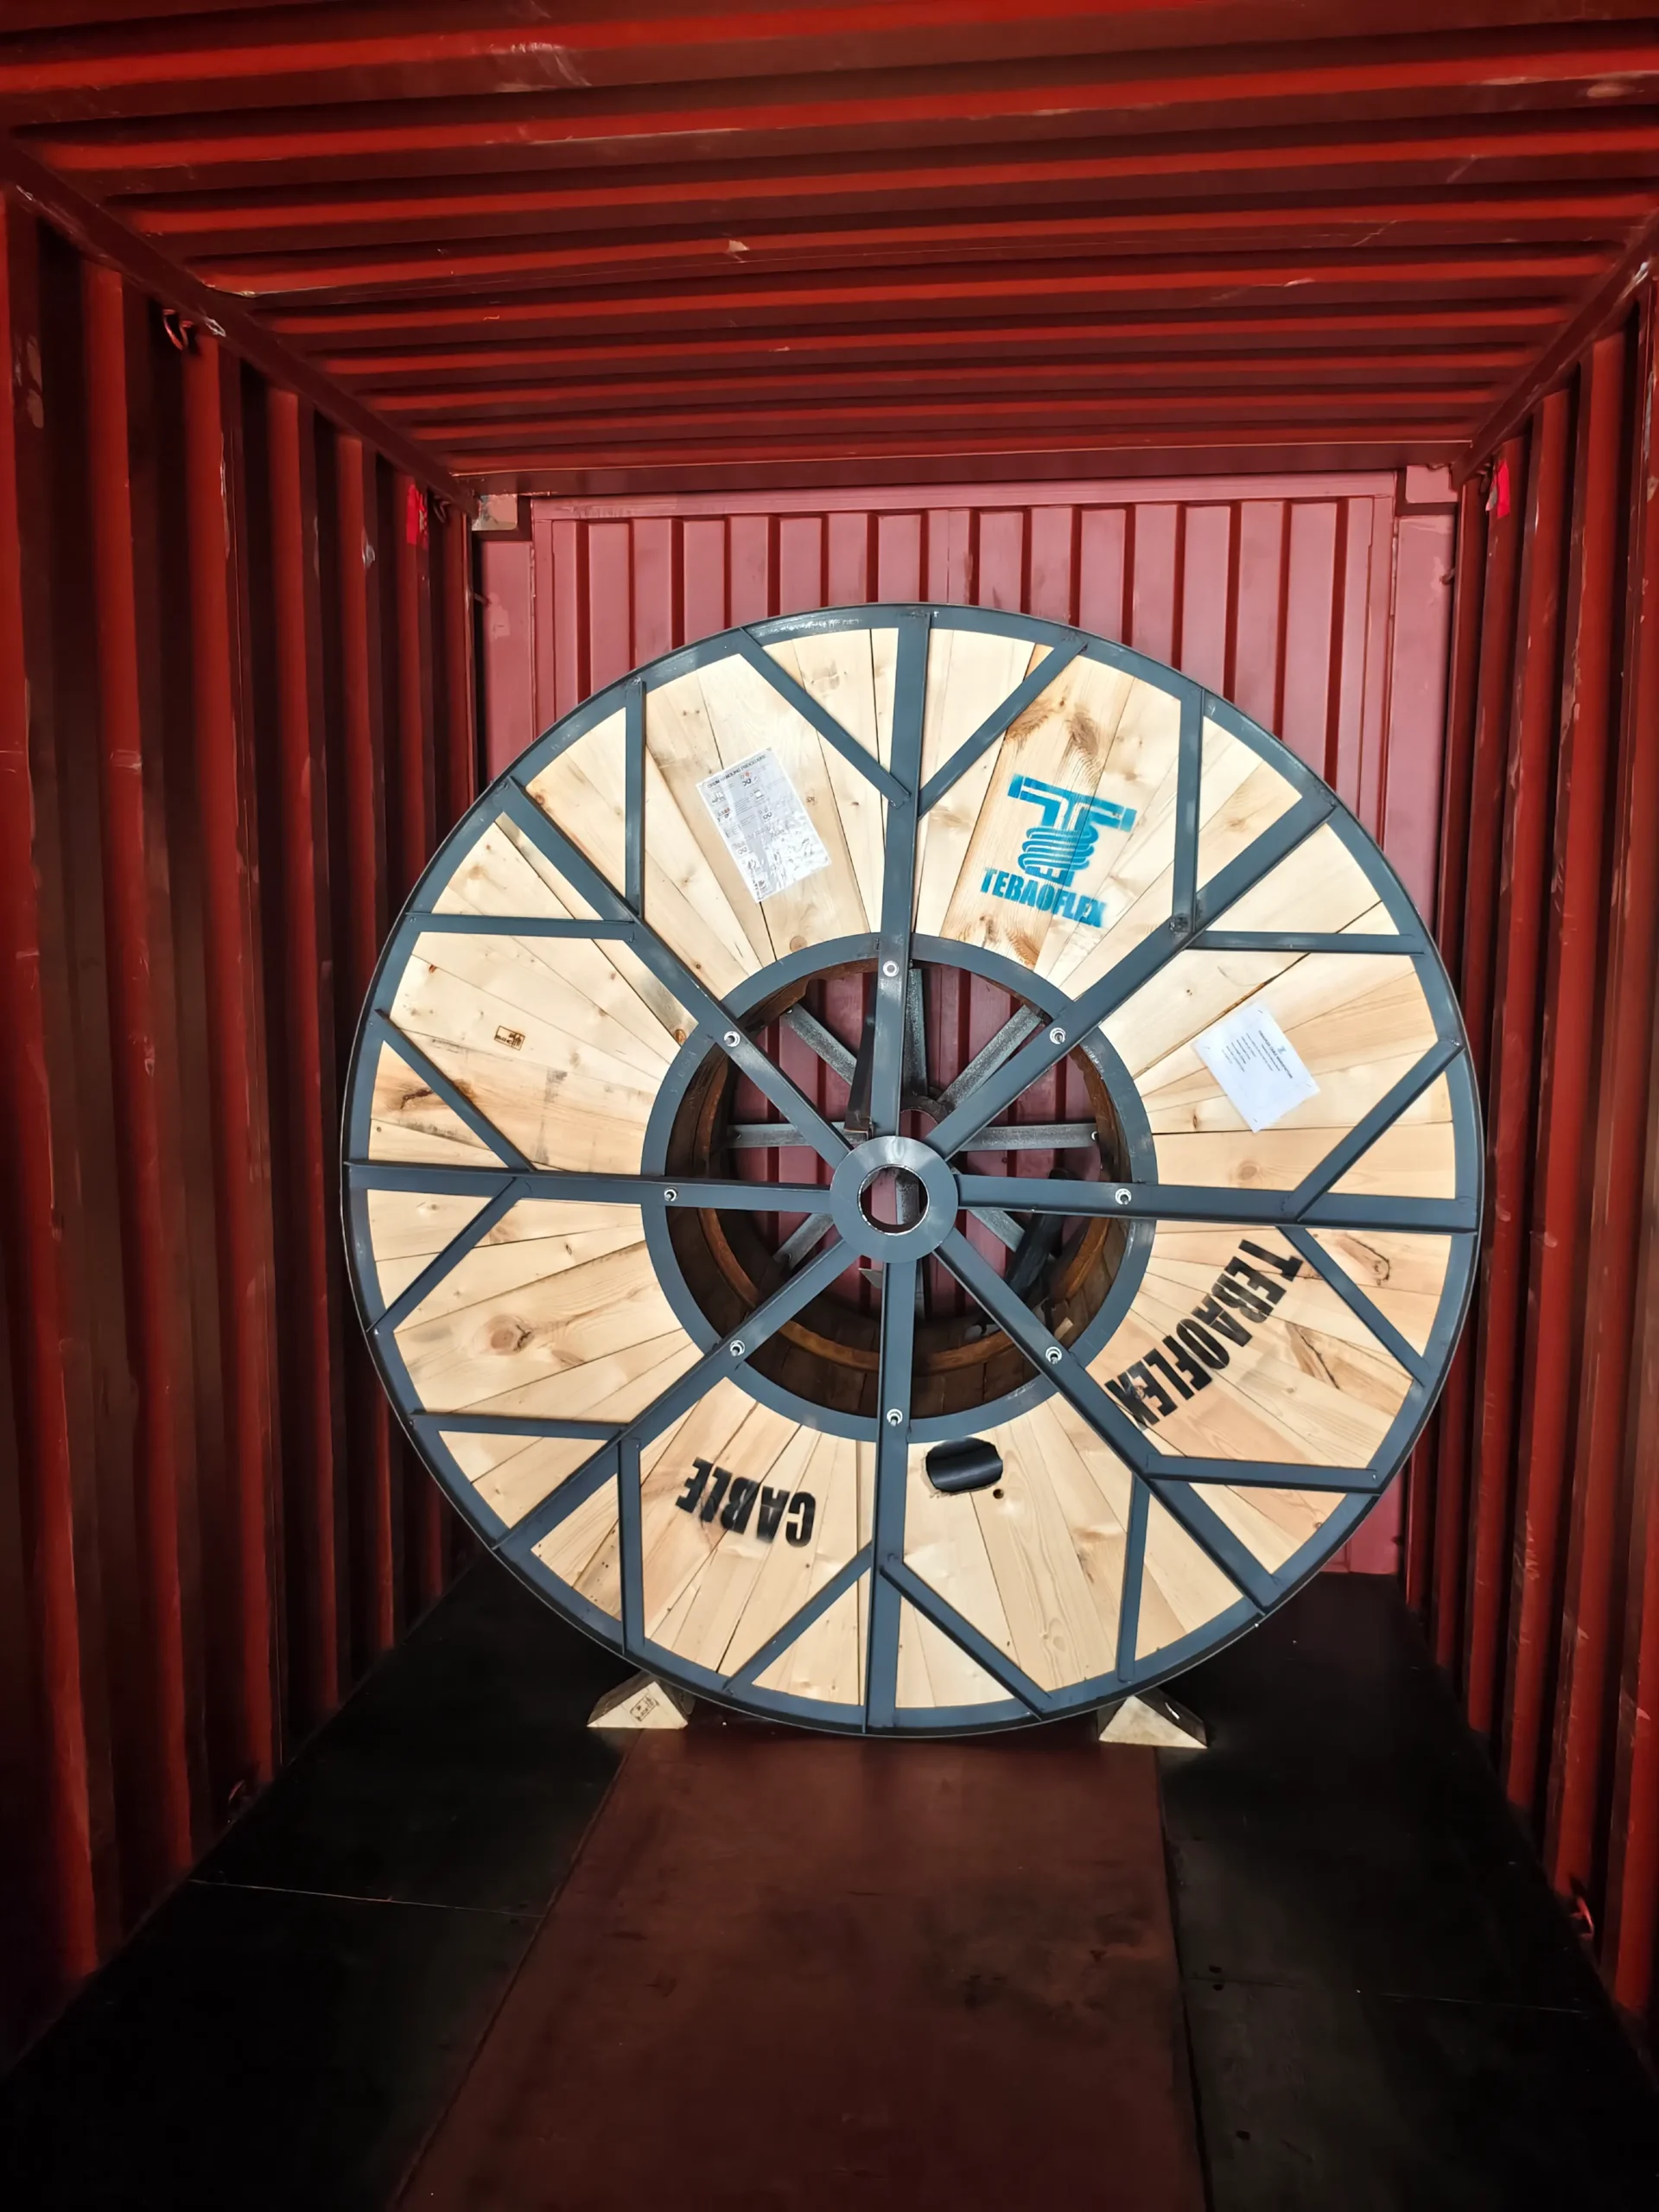
Fumigated wooden cable drums loaded and secured inside an export shipping container OEM Branding & Export Delivery

OEM Marking, Drum Packing & Global Shipping

We support cable distributors, EPC contractors, and equipment OEMs with customized outer jacket printing, sequential meter marks, weather-sealed drum packaging, and complete customs clearance documentation.

  • Custom sheath color (Yellow, Orange, Black, Red, Blue) & durable embossing/inkjet legend
  • ISPM-15 heat-treated fumigated wooden or steel-wood drums with waterproof lagging
  • Full export document set: Packing List, Commercial Invoice, CO, Form E & B/L

From Specification Review to Port Delivery in Four Steps

A structured four-stage engineering workflow ensures that electrical ratings, mechanical tolerances, sheath markings, and drum dimensions are locked in writing before raw copper stranding and rubber compounding begin.

STEP 01 Day 1

Requirement & Operating Load Intake

Submit your cable specification, equipment type, rated voltage, core × cross-section (mm²), order length, and operating environment (temperature, oil, water, or reeling speed).

Input: RFQ Data / Photos / Drawings
STEP 02 Within 24–48h

Datasheet & Drawing Sign-Off

TEBAOFLEX engineers prepare a project-specific technical datasheet detailing conductor stranding, insulation/sheath wall thickness, outer diameter tolerance, weight, and OEM sheath legend for your approval.

Deliverable: Signed Technical Datasheet
STEP 03 Production & QA

Manufacturing & Routine HV Inspection

Production proceeds through conductor bunching, rubber extrusion, continuous vulcanization (CV), braiding, and high-voltage spark/dielectric testing with full batch traceability records.

Deliverable: Routine Test Report & Photos
STEP 04 Dispatch

ISPM-15 Drum Packing & Export

Cables are wound to exact cut lengths per drum with sealed cable ends, custom metal/waterproof drum plates, container blocking reinforcement, and complete shipping documentation.

Deliverable: Drum List, CO & Bill of Lading
Need an urgent replacement cable for crane, mining, or marine maintenance? Send your existing cable marking or cross-section photo for a 24-hour engineering match and lead-time check.
Request 24h Engineering Review

Technical Documentation Package & Custom Order FAQ

Every custom or OEM cable order is supported by verifiable technical documentation required for EPC project submittals, distributor inventory registration, and international customs clearance.

Standard Project Document Deliverables

Prepared according to confirmed cable specifications and order terms:

Engineering Datasheet & Cross-Section Drawing Detailed dimensional table showing conductor stranding, insulation/sheath thickness, outer diameter tolerance, minimum bending radius, ampacity, and copper/total cable weight (kg/km).
Factory Routine Inspection & HV Test Report Drum-level test certificate recording 20°C conductor DC resistance, AC high-voltage withstand test, insulation resistance, and sheath tensile/elongation results.
International Compliance & System Certificates Copies of applicable TÜV Rheinland, VDE, UL/cUL, CE, KCS, Coal Mine Safety (MA), and ISO 9001 / ISO 14001 / ISO 45001 certificates.
Export Drum Schedule & Customs Clearance Set Net/gross weight per drum, drum flange dimensions, ISPM-15 fumigation certificate, Certificate of Origin (CO / Form E), Packing List, and Commercial Invoice.

Frequently Asked Questions on Custom Cable Orders

Direct answers for electrical engineers, OEM equipment builders, and overseas procurement teams:

Can TEBAOFLEX reverse-engineer a custom cable from our drawings, photos, or jacket markings?

Yes. You can send 2D drawings, existing cable sheath markings, cross-section photos, or equipment operating parameters. Our engineering team analyzes conductor class, insulation/sheath compounds, shielding, and tensile load requirements, then issues a matching or upgraded TEBAOFLEX specification datasheet within 24 hours.

What is the typical Minimum Order Quantity (MOQ) and lead time for custom cables?

MOQ depends on voltage rating and cross-section size. For common flexible rubber and control cables, standard specifications are often available from stock or with low trial MOQs (100 m to 500 m). Custom multi-core reeling, hybrid fiber-optic, or medium-voltage (3.6/6 kV to 35 kV) cables typically require 300 m to 1,000 m per production run, with standard manufacturing lead times of 10 to 25 working days.

Do you offer OEM private-label sheath printing and custom drum lengths?

Yes. We support custom outer sheath colors, continuous inkjet or embossed brand/specification legends, sequential meter marking (001m to end), custom drum flange markings, and project-specific cut lengths per reel (e.g., 250 m, 500 m, or exact crane reel lengths) to eliminate field splicing.

Can we request physical cable samples before placing a bulk project order?

Yes. For stocked or active production models, we provide short physical cable samples (typically 30 cm to 1 m) free of charge so your engineers can inspect conductor stranding flexibility, insulation thickness, braiding density, and outer sheath compound quality prior to bulk purchase.

What technical parameters should we include when requesting a custom cable quotation?

To receive the fastest accurate quote, please share: (1) Application equipment and movement type (fixed, trailing, festoon, or motorized reeling); (2) Rated voltage (e.g., 450/750 V, 0.6/1 kV, 6/10 kV); (3) Number of cores × nominal cross-section (mm²); (4) Environmental exposure (ambient temperature range, oil, water depth, or abrasion); and (5) Total quantity, preferred drum cut lengths, and destination port.

How are heavy-duty cables packaged and protected for long-distance sea freight?

All export cables are wound onto ISPM-15 heat-treated fumigated wooden drums or reinforced steel-wood drums. Both cable ends are hermetically sealed with heat-shrink caps to prevent moisture ingress at sea, wrapped in protective PE film and external wooden battens, and secured inside containers with timber chocks and tension straps.

Ready to Specify Your Custom Industrial Cable Project?

Send your specification list, equipment parameters, or cable photos to our engineering desk. We will reply within 24 hours with a confirmed structure datasheet, factory lead time, and FOB/CIF quotation.

  • ✓ Application & Voltage Rating
  • ✓ Cores × Cross-Section (mm²)
  • ✓ Total Length & Drum Cut Rules
  • ✓ Drawings or Sheath Markings